

Description
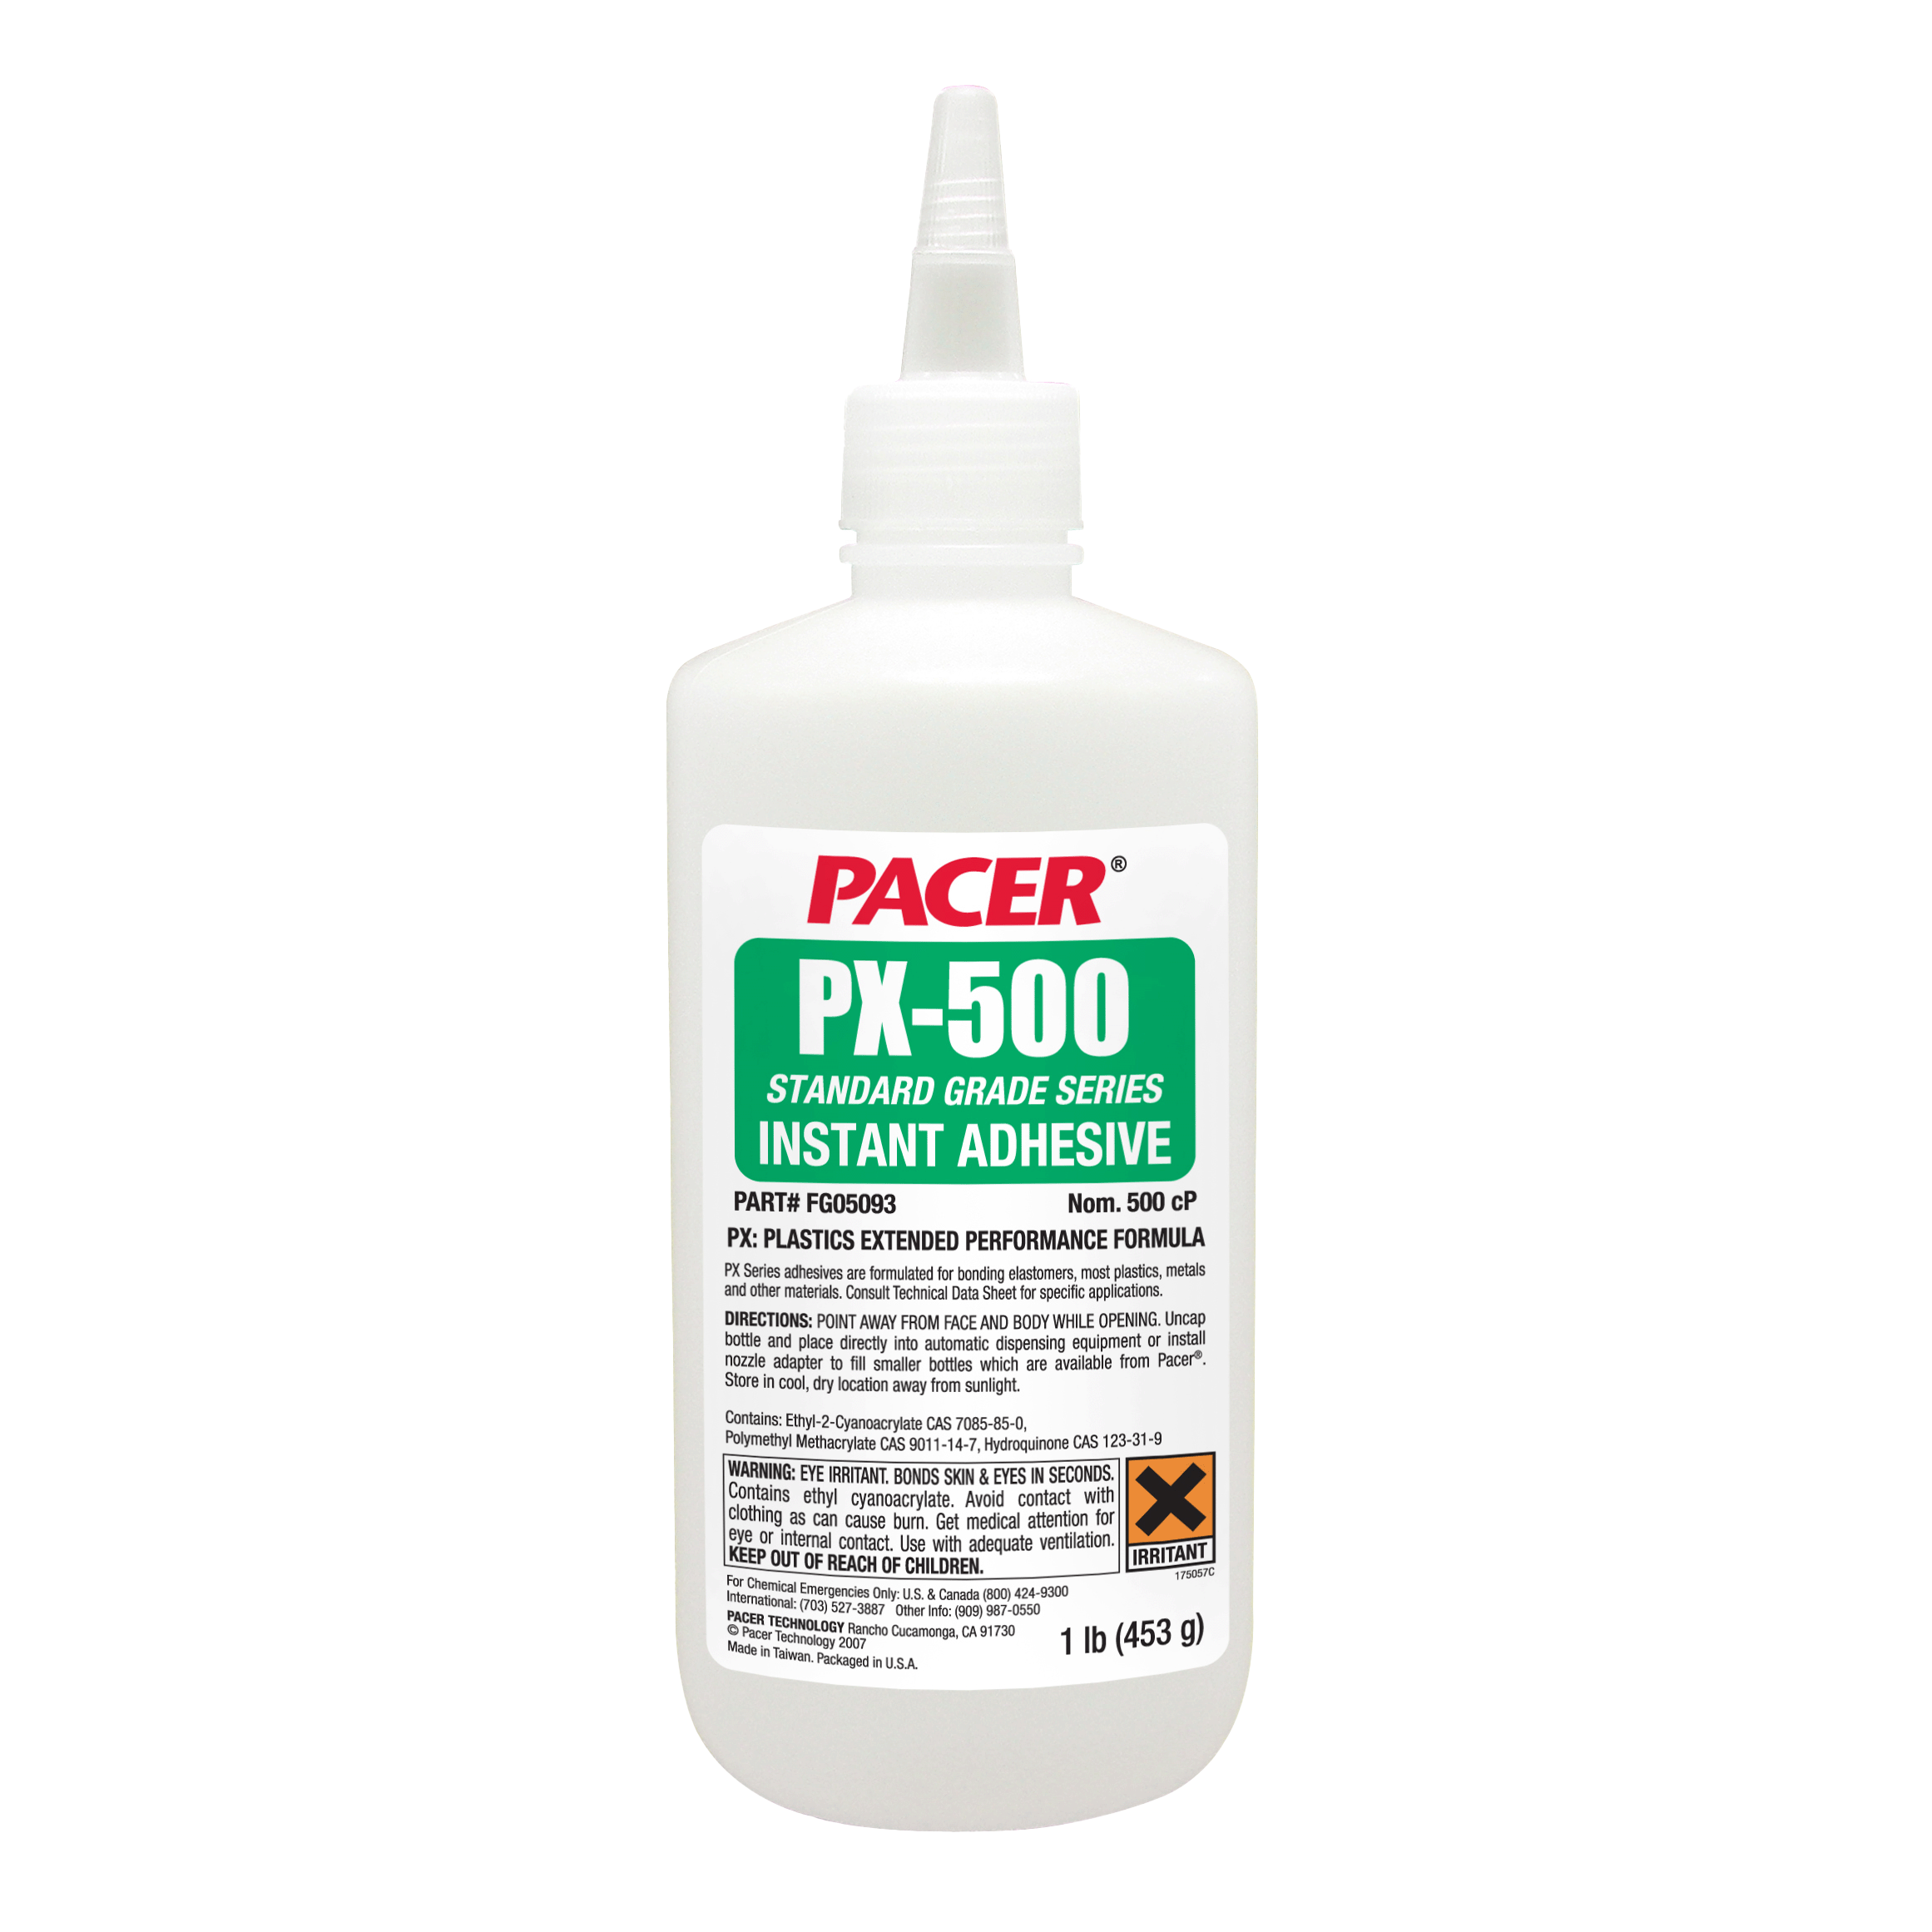
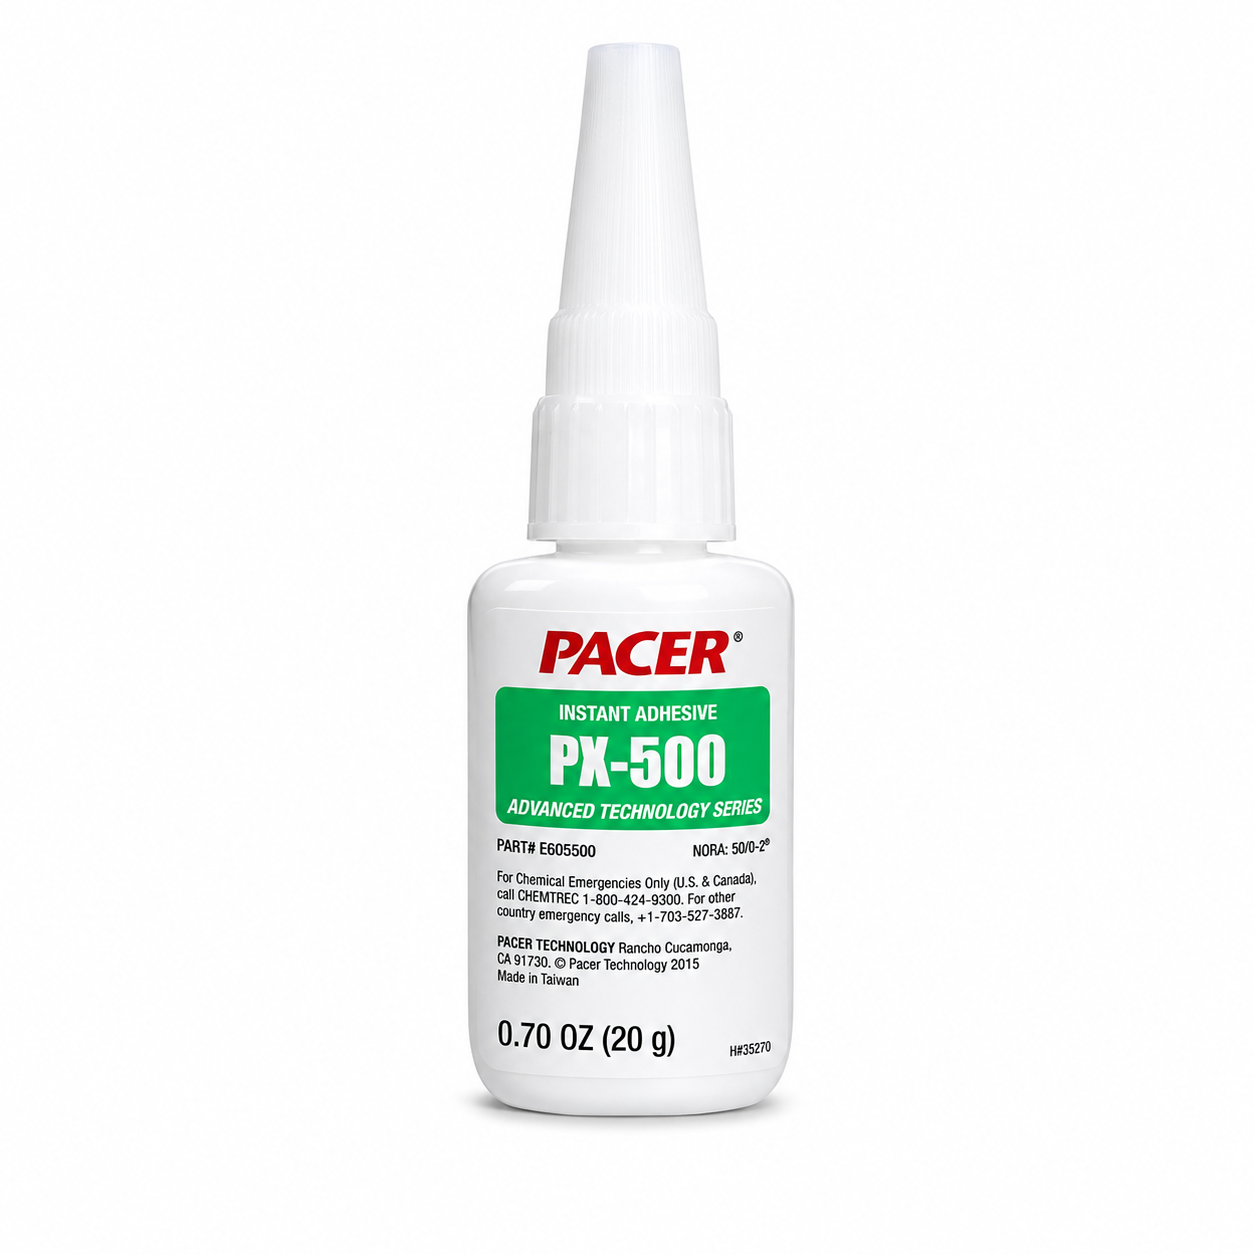
Pacer PX-500 cyanoacrylate is a one-component instant adhesive formulated for bonding many plastics and elastomers. Its slower fixture profile gives assemblers more time to align parts than a very fast, low-viscosity grade, while the 500 cP viscosity helps the liquid remain in controlled bond areas and bridge gaps up to 0.008 inch.
Cyanoacrylate Assembly for Plastic and Rubber Parts
PX-500 suits production work where fit, orientation, or cosmetic alignment must be checked before the joint locks in place. The medium-viscosity liquid can be applied as a small bead or controlled drop to close-fitting surfaces. It is useful for molded plastic components, elastomer details, housings, trim, and other assemblies that need rapid one-part bonding without meter-mix equipment.
Instant-adhesive performance depends on the exact resin, rubber compound, surface condition, and joint design. Clean both mating surfaces and remove oil, dust, release agent, and loose contamination. Apply only enough adhesive to wet the bond line, join the parts promptly, and hold the alignment until handling strength develops. Testing on the actual production materials is important, especially with low-surface-energy plastics, plasticized materials, or parts exposed to heat, moisture, cleaners, or repeated flexing.
Cyanoacrylate Handling and Application Details
The PX series technical sheet identifies PX-500 as the slowest and highest-viscosity option in the family. The longer positioning window can reduce scrapped assemblies when operators must seat clips, align edges, or confirm a precise orientation. The viscosity also helps limit uncontrolled run-off compared with thinner instant adhesives. Bond-line thickness should still remain small because instant adhesives perform best in close-fitting joints.
Dispense from a clean tip and keep the nozzle free of cured material. Avoid touching the tip to a contaminated surface because debris or moisture can shorten storage life inside the bottle. Cap the container promptly after use. Adhesive selection should account for substrate chemistry, gap size, required fixture speed, and service exposure rather than viscosity alone.
Joint design has a direct effect on results. Provide enough overlap to carry the expected load and avoid peel forces that concentrate stress at one edge. Fixtures should hold the parts without shifting while the adhesive develops handling strength. On visible assemblies, trial the dispense volume so squeeze-out stays away from finished surfaces. When a primer is required for a difficult plastic, qualify the primer, adhesive, and application sequence together. Document the accepted drop size, open time, clamping method, and inspection point so different operators reproduce the same bond. A controlled process also makes it easier to distinguish a material problem from a preparation or dispensing problem.
Specifications
| Property | Value |
|---|---|
| SKU | PAC-FG05093 |
| Brand | Pacer Technology |
| Product family | PX Series |
| Chemistry | Cyanoacrylate |
| Viscosity | 500 cP |
| Gap fill | Up to 0.008 inch |
| Package | 1 lb bottle |
| Components | One component |
For related grades, primers, debonders, and application accessories, browse instant adhesives. Product family information is available from The Original Super Glue Corporation. Confirm material compatibility and fixture time with a representative assembly before releasing a production process.
Need Help?
Need help matching viscosity and fixture speed to a plastic or elastomer joint? Call (800) 220-1966 or email [email protected].


Reviews
There are no reviews yet.