

Description
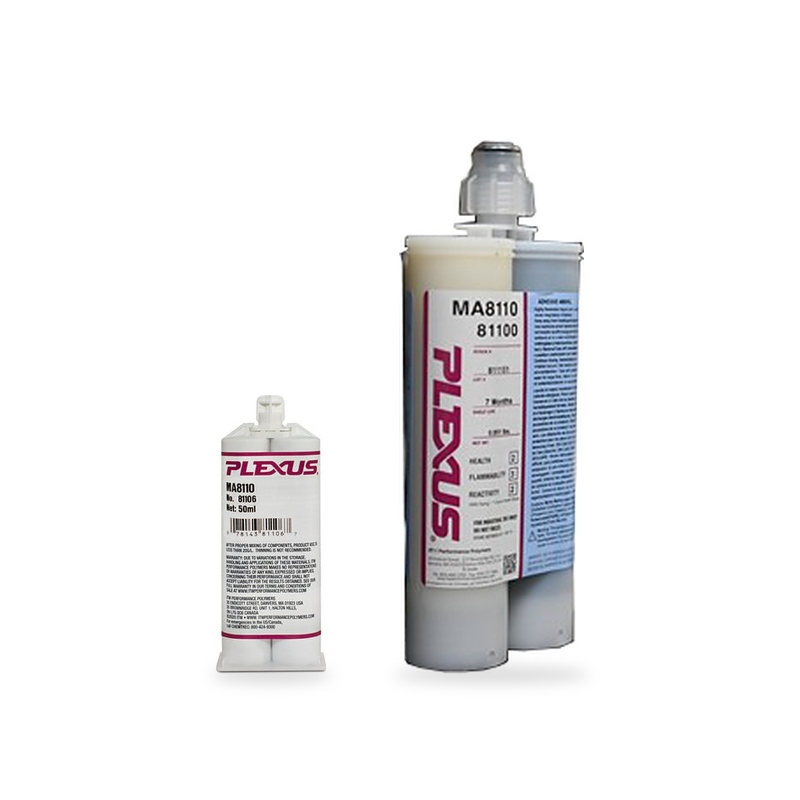
Plexus MA8110 GB is a two-part, 1:1 methacrylate (MMA) structural adhesive from ITW Performance Polymers, made in the USA. ITW designed it primarily for bonding galvanized coated metals, in particular hot dipped G90 and G60, and it also bonds raw metals, engineered thermoplastics, and composites with little to no surface preparation. Of the three MA8000 GB grades, MA8110 GB sits in the middle on working time, which gives you more time to position parts than MA8105 GB without the long wait of MA8120 GB.
The adhesive dispenses as a non-sagging gel through a static mix nozzle, and the glass beads in the formula hold a consistent bondline while parts are clamped. You lay a bead on one part, join the parts inside the working time, and hold them until the bond reaches handling strength. It is also supplied in 5 gallon pails and 50 gallon drums for bulk meter, mix, and dispense equipment.
Key Product Details
| Property | Value |
|---|---|
| Chemistry | Two-part methacrylate (MMA) structural adhesive, low halogen |
| Mix Ratio | 1:1 by volume (1.01 to 1.00 by weight, Part A to Part B) |
| Color | Gray (Part A off-white, Part B gray) |
| Consistency | Non-sagging gel |
| Glass Bead Spacers | 0.012 in (0.3 mm) inert glass beads |
| Viscosity | Part A 40,000 to 80,000 cP, Part B 40,000 to 80,000 cP |
| Density | Part A 0.97 g/ml, Part B 0.96 g/ml |
| VOCs During Cure | Less than 0.5% |
| Peak Exotherm Time (10 g) | 16 to 20 min |
| Peak Exotherm Temperature (10 g) | About 283°F (141°C) |
| Gap Tolerance | 0.01 to 0.5 in (0.25 to 12.7 mm) |
| Hardness | 74 Shore D |
| Tensile Strength | 3,285 to 4,015 psi (22.7 to 27.2 MPa) |
| Tensile Modulus | 170 to 230 kpsi (1,172 to 1,586 MPa) |
| Elongation at Break | 25 to 45% |
| Operating Temperature | -40°F to 180°F (-40°C to 82°C) |
| Recommended Application Temperature | 65°F to 85°F (18°C to 30°C) |
| Shelf Life | 12 months |
| Storage | 55°F to 77°F (13°C to 25°C) continuous storage |
| Country of Manufacture | USA |
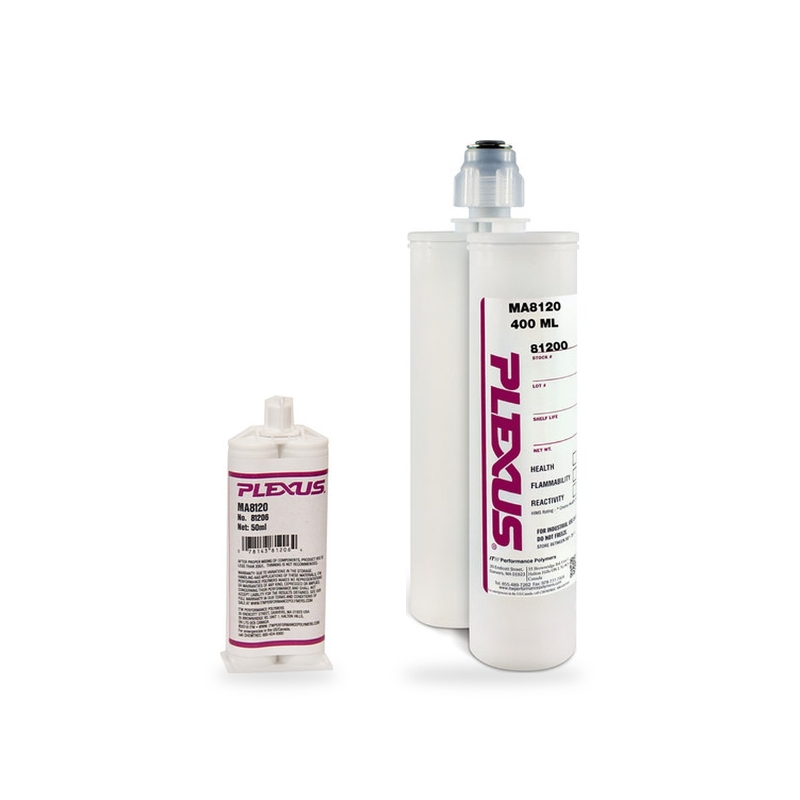
| Available Sizes | 50ml cartridge, 400ml cartridge, 5 gallon pail, 50 gallon drum |
Typical values from the ITW Performance Polymers technical data sheet last updated 12/20/2023. Tensile tested to ASTM D638 / ISO 527. Operating temperature is from the ITW MA8000 GB series sheet.
Cure Time by Temperature
| Temperature | 60°F (15.6°C) | 75°F (23.9°C) | 90°F (32.2°C) |
|---|---|---|---|
| Work Time, min | 12 to 14 | 8 to 12 | 6 to 8 |
| Time to 50 psi (0.3 MPa), min | 38 to 44 | 33 to 36 | 25 to 30 |
| Time to 500 psi (3.4 MPa), min | 45 to 55 | 35 to 40 | 30 to 35 |
| Time to 1000 psi (6.9 MPa), min | 65 to 85 | 44 to 50 | 35 to 40 |
Lap Shear Strength by Substrate
| Substrate | Lap Shear, psi (MPa) | Failure Mode |
|---|---|---|
| Aluminum | 3,061 (21.1) | Cohesive failure |
| Stainless steel | 2,800 (19.3) | Cohesive failure |
| Carbon steel | 2,800 (19.3) | Cohesive failure |
| Galvanized steel | 2,215 (15.3) | Substrate failure |
| ABS sheet | 700 (4.8) | Substrate failure |
| Fiberglass reinforced plastic (FRP) | 700 (4.8) | Substrate failure |
| PVC | 650 (4.5) | Substrate failure |
| Gel coat | 568 (3.9) | Substrate failure |
Tested to ASTM D1002. Cohesive failure means the adhesive failed within itself and the bond stayed on the metal. Substrate failure means the substrate gave out before the bond did, so the number reflects the substrate, not the adhesive.
Performance in Production
- An 8 to 12 minute working time at 75°F leaves room to position larger or multi-point assemblies, and the bond reaches 500 psi in 35 to 40 minutes. Stations that join parts right after dispensing can use MA8105 GB, and assemblies that need more time can use MA8120 GB.
- Temperature moves the cure. Cold stretches the working time and heat shortens it, so hold material and shop temperature steady through the year to keep mixing and cure consistent.
- The 0.012 in glass beads keep a consistent bondline when parts are clamped under pressure.
- The non-sagging gel stays where it is laid on vertical and overhead joints, and the 0.01 to 0.5 in gap tolerance covers fit-up variation on formed and fabricated parts.
- The 1:1 ratio is easy to meter, and ITW notes the system handles off-ratio mixing. Dispense only what you can use inside the working time, because large masses of mixed material build heat fast.
- A bonded joint spreads load along the whole bond line, and ITW notes it lowers the galvanic corrosion risk that comes with joining dissimilar metals with fasteners.
- Service range runs from -40°F to 180°F. Strength changes with temperature, so check the strength retention curve in the technical data sheet for your service range.
- ITW rates the cured adhesive excellent against hydrocarbons, acids and bases (pH 3 to 10), and salt solutions. ITW lists strong polar solvents, strong acids, and bases as the ones it is susceptible to.
Common Applications
- Structural bonding of hot dipped G90 and G60 galvanized steel assemblies without a primer
- Galvanized steel bonded to aluminum, stainless steel, plastics, or composites
- HVAC sheet-to-post and bracket bonding, and weld replacement
- Sign fabrication, including channel letters, structure and support, and lighting accessories
- Furniture assembly with mixed materials, including legs and hardware
- Bonding ABS, PVC, FRP, and gel coat parts to metal
- Metal-to-rubber and plastic-to-rubber joints
- Production lines running meter, mix, and dispense equipment from 5 gallon pails or 50 gallon drums
Available Sizes
| Size | Chemical Concepts SKU | ITW Stock No. |
|---|---|---|
| 50ml Cartridge, 1:1 | PLX81111 | 81111 |
| 400ml Cartridge, 1:1 | PLX81108 | 81108 |
| 5 Gallon Pail, Adhesive | PLX81101 | 81101 |
| 5 Gallon Pail, Activator | PLX81103 | 81103 |
| 50 Gallon Drum, Adhesive | PLX81102 | 81102 |
| 50 Gallon Drum, Activator | PLX81104 | 81104 |
Pails and drums are sold as adhesive and activator, and the two mix 1:1 by volume, so order matching quantities of each. The 5 gallon and 50 gallon adhesive is the same for MA8110 and MA8120, and the activator sets the grade, so order the MA8110 activator for MA8110. The pail and drum adhesive listed here is the version without glass beads. Call us if you need bulk adhesive with glass beads.
Plexus MA8000 GB Series Comparison
MA8105 GB, MA8110 GB, and MA8120 GB are the same 1:1 methacrylate platform in three working times. All three use 0.012 in glass beads, a 0.01 to 0.5 in gap tolerance, and the same cartridge sizes and guns.
| Property | MA8105 GB | MA8110 GB (this page) | MA8120 GB |
|---|---|---|---|
| Mix Ratio | 1:1 | 1:1 | 1:1 |
| Work Time at 75°F | 3 to 6 min | 8 to 12 min | 18 to 22 min |
| Handling Time at 75°F (time to 50 psi) | 12 to 14 min | 33 to 36 min | 50 to 60 min |
| Tensile Strength | 3,285 to 4,015 psi (22.7 to 27.2 MPa) | 3,285 to 4,015 psi (22.7 to 27.2 MPa) | 2,907 to 3,630 psi (20.5 to 25.0 MPa) |
| Tensile Elongation | 5 to 10% | 25 to 45% | 30 to 60% |
| Lap Shear on Aluminum | 2,694 psi (18.6 MPa) | 3,061 psi (21.1 MPa) | 2,906 psi (20.0 MPa) |
| Lap Shear on Galvanized Steel | 2,178 psi (15.0 MPa), G70 | 2,215 psi (15.3 MPa) | 2,656 psi (18.3 MPa), G90 |
| Viscosity, Part A / Part B | 70,000 to 140,000 / 50,000 to 120,000 cP | 40,000 to 80,000 / 40,000 to 80,000 cP | 40,000 to 80,000 / 80,000 to 120,000 cP |
| Operating Temperature | -40°F to 180°F (-40°C to 82°C) | -40°F to 180°F (-40°C to 82°C) | -40°F to 180°F (-40°C to 82°C) |
| ITW Stock No., 50ml / 400ml | 81057 / 81058 | 81111 / 81108 | 81211 / 81208 |
Values from the ITW technical data sheets (MA8105 GB dated 03/04/2025, MA8110 GB and MA8120 GB dated 12/20/2023) and the ITW MA8000 GB series sheet for operating temperature. Lap shear is tested to ASTM D1002. The MA8110 GB galvanized result ended in substrate failure, and the others ended in cohesive failure. Handling time is the time to 50 psi.
Related Products
- Plexus MA8105 GB: same 1:1 platform with a 3 to 6 minute working time at 75°F
- Plexus MA8120 GB: same 1:1 platform with an 18 to 22 minute working time at 75°F
- 50ml cartridge guns: Chem-Set PAK-50 manual dispense gun or Chem-Set PAK-50 electric battery dispense gun
- 50ml cartridge static mixer: MAQ 05-24L Quadro mixer
- 400ml cartridge guns: Albion B26T400 manual gun or medmix DP2X 400 pneumatic gun
- 400ml cartridge static mixer: MCQ 08-24T Quadro mixer
How to Bond with Plexus MA8110 GB
Bonding galvanized steel and other substrates with MA8110 GB follows the same shop sequence on every joint. This is the process from the ITW technical data sheet.
- Check temperature. ITW recommends applying the adhesive between 65°F and 85°F. Outside that range the cure slows down or speeds up significantly.
- Prepare the surfaces. Keep them free of grease, dirt, and other contaminants. On plastics, coated metals, and raw metal, a wipe with a dry rag or light solvent may be enough. Heavily oxidized or contaminated metal may need abrasion and cleaning. Dust-free composites can be bonded as is, or abraded lightly to remove mold release.
- Load the cartridge into the gun and remove the end caps. For pails and drums, use bulk meter, mix, and dispense equipment.
- Attach a static mix nozzle and expel a mixer length of adhesive before you apply to the part.
- Apply adhesive to one substrate. Use enough material to fill the joint completely when the parts are mated.
- Mate the parts inside the working time, 8 to 12 minutes at 75°F.
- Hold the parts in position until the bond reaches the strength you need to handle them. Keep the gap at or under 0.5 in.
- Clean up before the adhesive cures. Common lab solvents, citrus terpene or NMP cleaners, or soap and water work. Cured material comes off by careful scraping followed by a wipe with a cleaning agent.
ITW recommends testing your own materials to confirm the surface preparation. ITW lists these substrates for MA8110 GB:
- Raw metals: aluminum, stainless steel, raw steel
- Coated metals: hot dipped galvanized (G90 and G60), electrogalvanized, powder-coated, e-coated
- Thermoplastics: ABS and ABS blends, acrylics, polyamides (nylons), PBT, polycarbonate, rigid PVC, TPU
- Composites: DCPD, FRP, gelcoat, phenolics, epoxy-based composites, RIM
- Rubber
The lap shear table above covers the substrates ITW tested for this grade. For rubber compounds, nylon, and any substrate not in that table, call us before you commit to production.
Bulk Dispensing from Pails and Drums
The 5 gallon pails and 50 gallon drums run on bulk meter, mix, and dispense equipment, which ITW says can be applied manually or pneumatically. Automation is available from a variety of equipment manufacturers. ITW sets these requirements for the equipment:
- Bulk equipment must be explosion proof.
- Parts in direct contact with the liquid adhesive and activator should be stainless steel.
- Avoid brass, carbon steel, copper, and copper-containing alloys in fittings and pumps.
- Make seals and gaskets from Teflon, Teflon-coated PVC foam, ethylene/propylene, or polyethylene.
- Avoid Viton, BUNA-N, Neoprene, and other elastomers for seals and gaskets.
Plexus MA8110 Introduction Video
ITW Performance Polymers introduction to Plexus MA8110.
Frequently Asked Questions
What is Plexus MA8110 GB used for?
Plexus MA8110 GB is used for structural bonding of galvanized metal assemblies, and ITW designed it primarily for hot dipped G90 and G60 galvanized steel. It also bonds raw metals, engineered thermoplastics, and composites in industrial manufacturing, where an adhesive can take the place of welds or mechanical fasteners. ITW’s application sheets cover HVAC sheet-to-post and bracket bonds, sign structures, and furniture assemblies. Common Applications above has the full list.
Does Plexus MA8110 GB bond G90 and G60 galvanized steel?
Yes, MA8110 GB is the Plexus grade ITW designed primarily for hot dipped G90 and G60 galvanized steel, and it bonds galvanized steel without a primer. The ITW data sheet reports 2,215 psi lap shear on galvanized steel with substrate failure, meaning the substrate gave way before the bond did. ITW also lists electrogalvanized steel on its substrate list. MA8105 GB and MA8120 GB are the same platform with a shorter and a longer working time.
Does Plexus MA8110 GB bond plastics, nylon, and rubber?
Yes, MA8110 GB bonds engineered thermoplastics and composites with little to no surface preparation. In the data sheet, ABS and FRP tested at 700 psi, PVC at 650 psi, and gel coat at 568 psi, all with substrate failure, so the plastic or composite gave out before the bond did. ITW also lists nylon (polyamide) and rubber as substrates, but the data sheet has no nylon or rubber lap shear for this grade. If nylon is your main substrate, look at MA8105 GB. For rubber compounds and any plastic not on the list, call us.
Is MA8110 the same as MA8110 GB, and where is it made?
Yes, MA8110, MA8110GB, and MA8110 GB are the same adhesive, and GB means it contains glass bead spacers. ITW supplies the 50ml and 400ml cartridges only with the glass beads. Bulk pails and drums come with or without them. MA8110 GB is made in the USA.
How long is the working time and how fast does MA8110 GB cure?
At 75°F the working time is 8 to 12 minutes and the bond reaches 500 psi in 35 to 40 minutes. Cold slows the cure and heat speeds it up. At 60°F working time runs 12 to 14 minutes, and at 90°F it drops to 6 to 8 minutes. The cure table above covers all three temperatures.
Do I need a primer or surface prep with MA8110 GB?
No primer is called for on the substrates ITW lists, and surface prep is usually light. Wipe plastics, coated metals, and raw metal with a dry rag or light solvent. Heavily oxidized or contaminated metal may need abrasion and cleaning, and composites may need light abrasion to remove mold release. ITW recommends testing your own materials to confirm the prep.
What gun, mixer, or equipment do I need for MA8110 GB?
The 50ml cartridge runs in the Chem-Set PAK-50 manual gun or the PAK-50 electric battery gun with a MAQ 05-24L mixer. The 400ml cartridge runs in the Albion B26T400 manual gun or the medmix DP2X 400 pneumatic gun with an MCQ 08-24T mixer. These are the same guns and mixers we pair with MA8105 GB and MA8120 GB. The 5 gallon pails and 50 gallon drums run on bulk meter, mix, and dispense equipment, and the Bulk Dispensing section above lists ITW’s equipment requirements.
How does MA8110 GB compare to MA8105 GB and MA8120 GB?
MA8105 GB, MA8110 GB, and MA8120 GB are the same 1:1 platform with the same glass bead spacers and gap tolerance, and they differ mainly in working time and elongation. At 75°F, MA8105 GB has a 3 to 6 minute working time, MA8110 GB has 8 to 12 minutes, and MA8120 GB has 18 to 22 minutes. MA8110 GB sits in the middle on elongation too. Pick by how long you need to position parts and how much the joint has to flex. The series comparison table above lines the key specs up side by side.
Questions on fit for your galvanized steel or mixed-material bonding job? Call (800) 220-1966 or email [email protected].


Reviews
There are no reviews yet.