

Description
Permabond TA4611 Overview
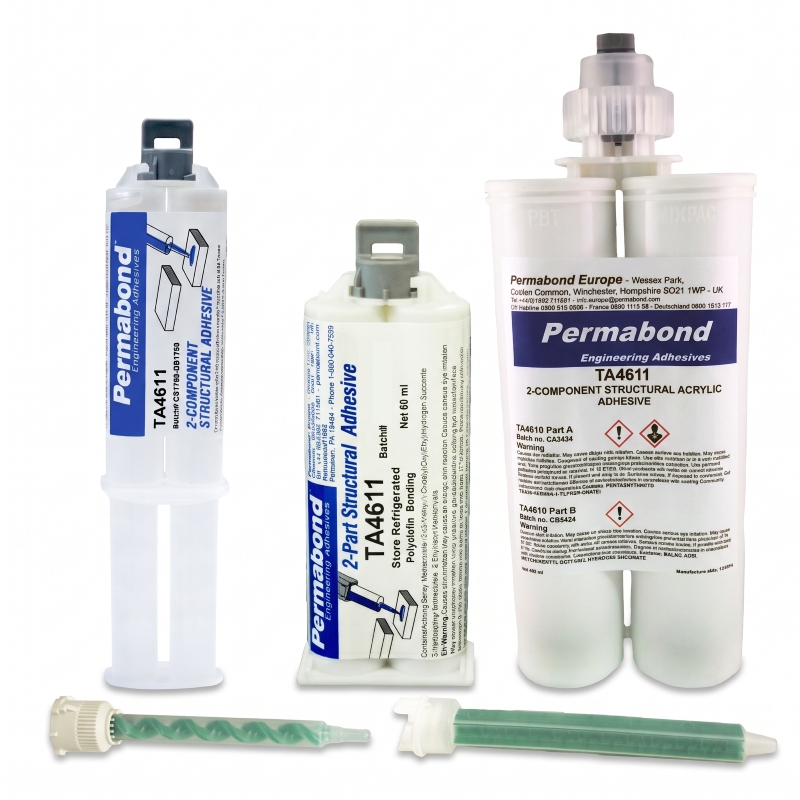
Permabond TA4611 is a two-part, 1:1 toughened structural acrylic (MMA) adhesive that bonds untreated low surface energy plastics including polypropylene, polyethylene (HDPE, LDPE, UHMW) and PTFE. No flame, corona, plasma or primer treatment is required before bonding.
TA4611 is similar to TA4610 but contains no micro beads, which makes it the grade for tight-fitting parts and thin bond lines. Where TA4605 and TA4610 use microparticles to hold a controlled gap, TA4611 lets parts close down to a bond line the joint design actually calls for. Maximum gap fill is 0.5 mm and mixed viscosity is 21,500 cP, roughly a tenth of TA4610.
TA4611 also publishes steel figures, at 11 N/mm² on mild steel and the highest stainless steel figure in the series at 9 N/mm², which makes it a documented choice when the joint is metal to metal or plastic to steel. Both parts are methacrylate based, solvent free, and non-hazardous for transport. Manufactured in Italy.
Which TA4600 Grade Do You Need?
All four grades bond the same difficult plastics. The choice comes down to how fast you need to fixture, how large the assembly is, and how much gap the joint has.
| Grade | Key Difference | Fixture Time | Full Cure | Mixed Viscosity | Max Gap | Sizes |
|---|---|---|---|---|---|---|
| TA4605 | Fastest fixture in the series | 5 to 10 minutes | 24 hours | 125,000 cP | 1 mm (0.04 in) | 50ml, 400ml, 20 kg bulk |
| TA4610 | Longer open time for large components, bonds underwater | 12 to 15 minutes | 48 hours | 210,000 cP | 1 mm (0.04 in) | 50ml, 400ml |
| TA4611 (this page) | No microbeads, for tight-fitting joints and thin bond lines. Highest stainless steel figure in the series | 10 to 16 minutes | 24 to 36 hours | 21,500 cP | 0.5 mm (0.02 in) | 25ml, 50ml, 400ml |
| TA4631 | No perceptible odor, no microbeads, bonds underwater | 12 to 18 minutes | 24 to 36 hours | 21,500 cP | 0.5 mm (0.02 in) | 25ml, 50ml, 400ml |
Choose TA4611 when the parts fit tightly and microparticles would hold the joint open, or when the joint involves steel. TA4611 and TA4631 are close in specification. Move to TA4631 if odor in the work area is the deciding factor, or if the bond will see water. See the full low surface energy plastic bonding guide for substrate-by-substrate selection.
Key Product Details
| Property | Value |
|---|---|
| Chemistry | Two-part toughened structural acrylic, methacrylate both parts |
| Mix Ratio | 1:1 |
| Color | Part A translucent, Part B transparent, mixed transparent to pale yellow |
| Viscosity at 25°C | Part A 20,000 to 30,000 mPa.s, Part B 10,000 to 15,000 mPa.s |
| Mixed Viscosity at 25°C | 21,500 cP |
| Specific Gravity | 1.0 (both parts) |
| Maximum Gap Fill | 0.5 mm (0.02 in). Contains no micro beads |
| Pot Life at 23°C | 4 to 6 minutes (2g + 2g) |
| Fixture Time at 23°C | 10 to 16 minutes |
| Handling Time at 23°C | 40 to 50 minutes |
| Working Strength at 23°C | 6 to 8 hours |
| Full Cure at 23°C | 24 to 36 hours |
| Temperature Exposure | -55°C minimum for the cured adhesive, depending on the materials bonded. Strength falls as temperature rises. Brief high-temperature excursions are acceptable if the joint is not unduly stressed |
| Surface Treatment Required | None. No primer, flame, corona or plasma treatment |
| Solvent Content | Solvent free |
| Transport Classification | Non-hazardous for transport |
| Country of Manufacture | Italy |
| Packaging | 25ml cartridge, 50ml cartridge, 400ml cartridge. Bulk available on request |
Shear Strength on Common Substrates
Tested per ISO 4587. An asterisk indicates the substrate failed before the bond line.
| Substrate | Shear Strength |
|---|---|
| Carbon Fibre | 14 N/mm² (2030 psi) |
| Epoxy FRP | 13 N/mm² (1885 psi) |
| Mild Steel | 11 N/mm² (1595 psi) |
| Polyester GRP | 10 N/mm² (1450 psi) |
| Stainless Steel | 9 N/mm² (1305 psi) |
| Polypropylene | >8 N/mm² (>1160 psi)* |
| HDPE | 8 N/mm² (1160 psi) |
| Mild Steel to PP | 8 N/mm² (1160 psi) |
| Mild Steel to HDPE | 8 N/mm² (1160 psi) |
| Stainless Steel to PP | 8 N/mm² (1160 psi) |
| Aluminium to PP | 8 N/mm² (1160 psi) |
| Aluminium to HDPE | 8 N/mm² (1160 psi) |
| Polyethylene | >7 N/mm² (>1015 psi)* |
| Stainless Steel to HDPE | 6 N/mm² (870 psi) |
| PTFE | >2 N/mm² (>290 psi)* |
| Mild Steel to PTFE | >2 N/mm² (>290 psi)* |
Nature of surface, surface preparation, glue line thickness, substrate thickness, pull speed, batch variation, cure time and temperature all affect shear strength measurement. Values are guideline figures, not a specification. TA4611 publishes 11 N/mm² on mild steel and 9 N/mm² on stainless steel. TA4631 is higher on mild steel at 14 N/mm², and TA4611 is higher on stainless. If the joint is metal to metal or plastic to steel, these two are the grades with the data behind them.
Performance in Production
- No micro beads means nothing holds the joint open. Parts can close to the bond line the design calls for, which matters on close-tolerance assemblies and visible joints.
- Maximum gap fill is 0.5 mm, half that of TA4605 and TA4610. If the joint has a real gap to fill, use one of those instead.
- At 21,500 cP mixed, TA4611 flows far more freely than TA4605 or TA4610. Plan to clamp or fixture vertical and overhead joints.
- Pot life is 4 to 6 minutes with fixture at 10 to 16 minutes. Enough time to position without the long clamp cycle of TA4610.
- Mixed color runs transparent to pale yellow rather than off-white.
- 1:1 mix ratio works with hand syringe on the 25ml, manual cartridge guns, pneumatic guns, and automated meter-mix equipment.
- Maintain clamp pressure until handling strength is reached at 40 to 50 minutes. Time varies with joint design and substrates.
- Adhesive squeezed outside a closed joint cures more slowly and may feel soft due to air contact. Material inside the joint cures solid.
- TA4611 can take brief high-temperature excursions such as paint baking and wave soldering provided the joint is not unduly stressed.
- Not recommended in contact with strong oxidizing materials. May affect some thermoplastics, so check substrate compatibility before production.
Common Applications
- Close-tolerance and tight-fitting plastic assemblies where microparticles would hold the joint open
- Visible and cosmetic joints where a thin, less noticeable bond line matters
- Metal to metal bonding on mild steel and stainless steel
- Bonding polyolefins to mild steel, stainless steel and aluminium
- Bonding untreated polypropylene, polyethylene, HDPE and UHMW parts
- Composite bonding on carbon fibre, epoxy FRP and polyester GRP
- PTFE bonding, including PTFE to mild steel
- Rubber bonding on EPDM, nitrile, neoprene and butyl rubbers
- Engineering plastic bonding on acetal (POM), PET-G, PET-P and PEEK. Permabond lists these across the series, with shear figures published on TA4631
- Small-part and electronics-adjacent assembly where the 25ml syringe format suits low-volume precision work
Sizes and Matching Dispensing Equipment
TA4611 cartridges need a matching 1:1 mixer. Ordering the wrong mixer is the most common reason a first trial fails, so use this table to match the package to the hardware.
| Package | Full Case Quantity | Static Mixer | Dispensing Gun |
|---|---|---|---|
| 25ml Cartridge | 15 | MBQ 05-16L | None required. Hand syringe format |
| 50ml Cartridge | 10 | MBQ 05-16L | Chem-Set PAK-50 with the 1:1 / 2:1 plunger |
| 400ml Cartridge | 6 | MFQ 08-24T | Albion B26T400 manual, or DP2X 400 pneumatic |
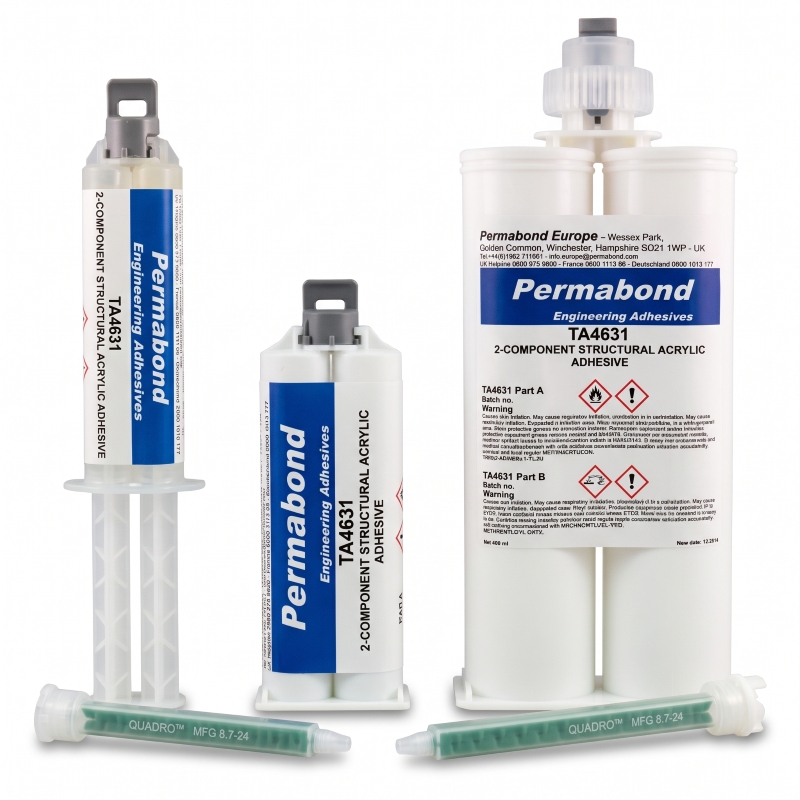
Every cartridge ships with one static mixer. Order spares separately, since each dispensing stop needs a fresh nozzle. The 25ml is a hand syringe and needs no gun, which makes it the easiest way to run a first trial. Cartridge sizes are total volume, split evenly between the two sides. Order single cartridges or full cases, whatever the job needs. Bulk packaging is available on request.
Storage and Handling
| Format | Storage Temperature |
|---|---|
| Cartridges | 5 to 25°C (41 to 77°F) |
| Bulk | 2 to 7°C (35 to 45°F) |
Bulk material requires refrigerated storage. The product may separate slightly in storage. Invert the container to re-disperse before use. For professional and industrial use only.
Related Products
- Permabond TA4631 for low-odor work areas and underwater bonding
- Permabond TA4605 for faster fixture and 1 mm gap fill
- Permabond TA4610 for large assemblies and underwater bonding
- MBQ 05-16L static mixers for 25ml and 50ml cartridges
- Chem-Set PAK-50 dispensing gun for 50ml cartridges
- MFQ 08-24T static mixers for 400ml cartridges
- Albion B26T400 manual gun for 400ml cartridges
- DP2X 400 pneumatic gun for 400ml production dispensing
- Low surface energy plastic bonding guide covering the full TA4600 series
How to Bond Untreated Polypropylene and HDPE With No Primer
Bonding untreated polypropylene or HDPE with TA4611 takes clean, dry parts, a static mixer and clamp pressure. No flame, corona or plasma step is needed on the plastic. The shop steps are below.
Surface preparation
- Surfaces must be clean, dry and grease-free before bonding.
- Molded polyolefin parts often carry residual mold release. Wipe with isopropanol (IPA) and let it fully evaporate before applying adhesive.
- On metals, aluminium and copper alloys benefit from light abrasion with emery cloth to remove the oxide layer. Worth doing on this grade given its steel performance.
- No primer, flame, corona or plasma treatment is required on the polyolefin side. That is the point of the TA4600 series.
Applying TA4611
- Confirm surfaces are clean, dry and grease-free.
- Apply a thin bead of adhesive pre-mixed through a static mixer nozzle.
- Assemble components and clamp.
- Maintain pressure until handling strength is achieved. Time varies with joint design and the surfaces being bonded.
- Allow 24 to 36 hours at 23°C for full cure.
The same process runs on polypropylene, HDPE, LDPE, UHMW and PTFE, and on polyolefin to steel, stainless steel, aluminium, e-coated metal and composites. Call us before you bond a substrate that is not listed on this page.
Frequently Asked Questions
Do I need to flame, corona or plasma treat the plastic first?
No. The TA4600 series was developed specifically to bond untreated polyolefin surfaces. No primer or pre-treatment is required. Surfaces still need to be clean, dry and grease-free, and molded parts should be wiped with IPA to remove mold release.
Is Permabond TA4611 an alternative to 3M Scotch-Weld DP8010?
Yes, as an alternative, not an equivalent. TA4611 is a two-part acrylic that bonds untreated polypropylene and polyethylene with no primer, which is the job DP8010 is used for. The main change is mix ratio. TA4611 mixes 1:1 and 3M lists DP8010 at 10:1, so swap the 10:1 plunger in your 3M EPX gun for a 1:1 plunger (50ml cartridges only), or use our Chem-Set PAK-50 with the 1:1/2:1 plunger. The 25ml syringe needs no gun, which makes it the cheapest way to run a trial. Pot life, fixture time and cure profile differ too, so run a trial on your parts before you change a production process. The low surface energy plastic bonding guide compares all four TA4600 grades.
What does no micro beads actually mean for my joint?
TA4605 and TA4610 contain microparticles that hold a minimum bond line, roughly 1 mm. That is useful when you want a controlled gap, and a problem when parts are supposed to seat tight. TA4611 has none, so the parts close as designed. Maximum gap fill drops to 0.5 mm as a result.
What is the difference between TA4611 and TA4631?
They are close. Both skip the micro beads, both run 21,500 cP mixed with a 0.5 mm gap, and both cure in 24 to 36 hours. TA4631 has no perceptible odor, bonds underwater and is stronger on mild steel (14 vs 11 N/mm²). TA4611 is stronger on stainless steel (9 vs 6 N/mm²) and fixtures slightly faster at 10 to 16 minutes versus 12 to 18. Pick TA4631 if odor, water exposure or mild steel decides it, TA4611 otherwise.
Which grade is best for bonding metal?
TA4631 is highest on mild steel at 14 N/mm² (2030 psi) and TA4611 is highest on stainless steel at 9 N/mm² (1305 psi). TA4611 publishes 11 N/mm² (1595 psi) on mild steel. TA4605 publishes no steel values at all. If the joint is metal to metal or plastic to steel, TA4611 or TA4631 are the documented choices.
Can TA4611 be used underwater?
The TA4611 data sheet does not list underwater bonding. TA4610 and TA4631 both list bonding underwater and water resistance as published features. Use one of those for submerged or wet-service joints.
What do I need to dispense the 25ml?
Nothing beyond the mixer that ships with it. The 25ml is a hand syringe format, so no gun is required. That makes it the simplest way to trial the product before committing to a cartridge size and dispensing equipment.
Where is Permabond TA4611 made?
Italy. TA4611 is manufactured in Italy and supplied in 25ml, 50ml and 400ml cartridges.
Questions on fit for your polyolefin bonding application? Call (800) 220-1966 or email [email protected].
3M, Scotch-Weld and EPX are trademarks of 3M Company. Permabond TA4600 series products are not made, sold or endorsed by 3M.


Reviews
There are no reviews yet.