

Description
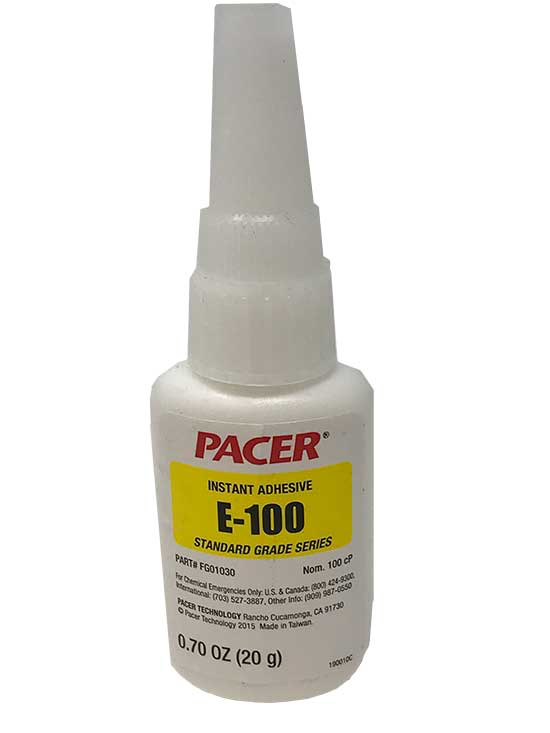
Pacer E-100 cyanoacrylate adhesive is a single component ethyl cyanoacrylate that runs 80 to 120 cP and fills to .005 in. It’s the middle grade in Pacer’s General Purpose E Series and the sensible default when you don’t have a reason to pick something else: thin enough to flow into a joint and wet both faces, thick enough that it doesn’t wick away and starve the bond line the way a 2 to 10 cP grade will, and the most forgiving gap of the thin and medium grades. At 80 to 120 cP it is still a flowing liquid, so plan on horizontal or clamped joints. E-100 bonds plastics, rubber, metal, and ceramic, fixtures in 1 to 5 minutes, and dispenses from the bottle or through automatic equipment. It meets MIL-A-46050C Type II, Class 2 and A-A-3097 Type II, Class 2.
Key Product Details
| Property | Value |
|---|---|
| Chemistry | Single component ethyl cyanoacrylate |
| Grade | General Purpose, E Series |
| Color | Clear transparent liquid |
| Viscosity | 80 to 120 cP |
| Typical Gap | .005 in |
| Fixture Time | 1 to 5 minutes |
| Strength Development | 80% of full strength in 15 to 30 minutes |
| Cured Temperature Range | -65F to +180F (-54C to +82C) |
| Heat Distortion | 250F / 121C |
| Softening Point | 306F / 153C |
| Glass Transition | 342F / 172C |
| Boiling Point | 365F / 185C |
| Flashpoint | 185F / 85C |
| Specific Gravity | 1.08 |
| Refractive Index | 1.45 (n20C/D, +/- .03) |
| Solubility Parameter | 10.7 |
| Vapor Pressure | 10 mm Hg at 70C |
| Volume Shrinkage | 13% |
| Rockwell Hardness | M 74 |
| Elongation | Less than 2% |
| Outgassing | 0 (at 10^-6 mmHg, 72F) |
| Dielectric Constant | 3.89 at 1 MHz |
| Volume Resistivity | 8.5 x 10^12 ohm-cm |
| Tensile, Steel | 4000 psi (+/- 10%), ASTM D2095 |
| Impact | 3 to 5 ft-lbs, ASTM 950 |
| Soluble In, Liquid State | Pacer X-9 Debonder, acetone, MEK, nitromethane |
| Soluble In, Cured State | Pacer X-9 Debonder, acetone, nitromethane |
| Specification Compliance | MIL-A-46050C Type II, Class 2; A-A-3097 Type II, Class 2 |
| Shelf Life | One year unopened, stored per the TDS |
| Country of Manufacture | USA |
| Available Sizes | 20 Gram (0.70 oz) Bottle, 1 lb (453 g) Bottle |
Full property data for every grade in the series is in the Pacer E Series technical data sheet (PDF). The data sheet covers grades and package sizes beyond what we currently stock. Of the E Series, Chemical Concepts carries E-5, E-40, E-100, and E-1500.
Tensile Shear Strength by Substrate
Tested per ASTM D1002. Where the table reads substrate failure, the part broke before the bond did.
| Substrate | Tensile Shear, psi (+/- 10%) |
|---|---|
| Steel | 2400 |
| Aluminum | 1600 |
| ABS | Substrate failure |
| Nylon | Substrate failure |
| Rigid PVC | Substrate failure |
| SBR | Substrate failure |
| EPDM | 100 |
How Cyanoacrylate Bonding Works
Cyanoacrylates cure by reacting with the trace surface moisture already on your parts. No mixing, no heat, no light. That’s why the process is fast and also why fit-up and cleanliness matter more than they do with a two part adhesive.
- Clean both faces. Oil, grease, mold release, and cutting fluid will all keep the bond from developing.
- Apply to one surface only. Applying to both just doubles the bond line and slows cure.
- Use as little as will wet the joint. One free-falling drop covers roughly one square inch of bond area, and a thinner bond line carries load better than a thick one.
- Mate the parts carefully and without delay, then hold. Excess squeeze-out is difficult to get off finished surfaces once it flashes over.
- Work flat or clamped where you can. E-100 flows, so on a vertical or overhead face it will move before it sets.
- Let it fixture for 1 to 5 minutes before handling, and give it 15 to 30 minutes to reach 80% of full strength before loading the joint.
- For gaps at the top of the range, a Pacer accelerator can drive cure through. Expect a possible white frost on exposed adhesive and a drop in overall cure strength when you use one.
Fixture and full cure both move with temperature, relative humidity, bondline thickness, and the substrate pair. Test on actual parts before you lock in a production process.
Choosing a Viscosity in the E Series
All four grades are the same ethyl cyanoacrylate chemistry. Viscosity is what changes, and it drives how much gap you can bridge, whether the adhesive stays put, and how strong the finished joint is.
| Grade | Viscosity | Typical Gap | Steel Shear | Impact | Best For |
|---|---|---|---|---|---|
| E-5 | 2 to 10 cP | .002 in | 2700 psi | 3 to 5 | Wicking into assembled joints |
| E-40 | 30 to 70 cP | .004 in | 2700 psi | 7 to 10 | Strongest grade in the series |
| E-100 | 80 to 120 cP | .005 in | 2400 psi | 3 to 5 | General purpose default, most forgiving gap of the thin grades |
| E-1500 | 1300 to 1700 cP | .010 in | 2200 psi | 4 to 6 | Looser fit-up and vertical joints, 20 gram only |
Two honest notes on that table. E-100 is the default, not the strongest: if your joint is loaded in tension or the finished part gets handled, E-40 gives 4700 psi tensile against E-100’s 4000 and more than double the impact strength, at the cost of .001 in less gap. And steel shear runs highest at the thin end of the series, because a thinner bond line carries load better than a thick one.
Outside the E Series: for a true gel that will not move at all on an overhead joint, see Pacer RX-50M Gel. For porous, acidic, or contaminated substrates where any standard cyanoacrylate struggles regardless of viscosity, Pacer RX-100 runs the same 80 to 120 cP in the non-surface-sensitive Range Extended chemistry. And if the joint sees real peel or repeated flexing, ask us about Pacer’s HP Series, which publishes T-Peel data the E Series does not.
Performance in Production
- At 80 to 120 cP E-100 flows into the joint and wets both faces without disappearing into the substrate, which is the trade you’re making against a 2 to 10 cP grade that penetrates further but leaves nothing in the bond line.
- .005 in gap capability is the most forgiving of the thin and medium grades, which is why this is the grade to stock when you’re bonding a mix of parts and don’t want to hold a viscosity for each one.
- Plan for a horizontal or clamped joint. This is a flowing liquid, not a gel, and it will run on a vertical or overhead face before it cures. Reorient the part, fixture it, or move up a grade.
- Fixture in 1 to 5 minutes and 80% of strength in 15 to 30 minutes means a bench operator can bond, set aside, and move a batch through inside one shift without a fixture bank tying up floor space.
- One drop per square inch of bond area makes a 20 gram bottle go a long way. Over-application does not add strength, it subtracts it and then squeezes out where you have to clean it.
- 2400 psi tensile shear on steel and 1600 psi on aluminum, with 4000 psi tensile on steel, puts E-100 in range for small metal parts where you’d otherwise reach for a mechanical fastener. If the joint needs more than that, E-40 is the stronger grade.
- On ABS, nylon, rigid PVC, and SBR the part failed before the bond in D1002 testing, so on those plastics your joint strength is set by the substrate, not the adhesive. EPDM is the exception at 100 psi and needs joint design and testing to match.
- Elongation under 2%, 13% volume shrinkage, and a 250F heat distortion point make this a rigid bond. Impact strength is 3 to 5 ft-lbs, the low end of the series, so it is not the pick for joints that flex, take shock, or run hot.
- Zero outgassing at 10^-6 mmHg, 8.5 x 10^12 ohm-cm volume resistivity, and a 3.89 dielectric constant give you published numbers to work from on vacuum and electrically sensitive assemblies.
Common Applications
- General purpose bonding of molded plastic parts in production assembly
- Rubber to metal and rubber to plastic bonding
- Small metal part bonding on steel and aluminum
- Ceramic bonding and repair
- Shops bonding a mix of parts that want one grade on the shelf rather than three
- Automated dispensing on production lines, or bottle dispensing at the bench
- Rework and repair of plastic, rubber, metal, and ceramic components
- Work calling out MIL-A-46050C Type II, Class 2 or A-A-3097 Type II, Class 2
- Vacuum and outgassing-sensitive assemblies, based on the published zero outgassing figure
Available Sizes
| Size | Net Weight | SKU | Pacer Part No. | UPC |
|---|---|---|---|---|
| 20 Gram Bottle | 0.70 oz (20 g) | PAC-FG01030 | FG01030 | 0 87093 00209 8 |
| 1 lb Bottle | 1 lb (453 g) | PAC-FG01033 | FG01033 | 0 87093 00210 4 |
The 20 gram is a stocked item. The 1 lb is a special order with a 10 to 15 day lead time, and special orders cannot be canceled or returned. If you buy the 1 lb on a repeating basis, call us about a standing order. If you need a smaller package than 20 gram, E-5 is the only grade in the current E Series offered in a 5 gram bottle.
Related Products
- Pacer E-5 Instant Adhesive (2-10 cP), water-thin wicking grade for already-assembled joints, .002 in gap, 5 gram, 20 gram, and 1 lb bottles
- Pacer E-40 Instant Adhesive (30-70 cP), strongest grade in the E Series, 4700 psi tensile and 7 to 10 ft-lbs impact, .004 in gap
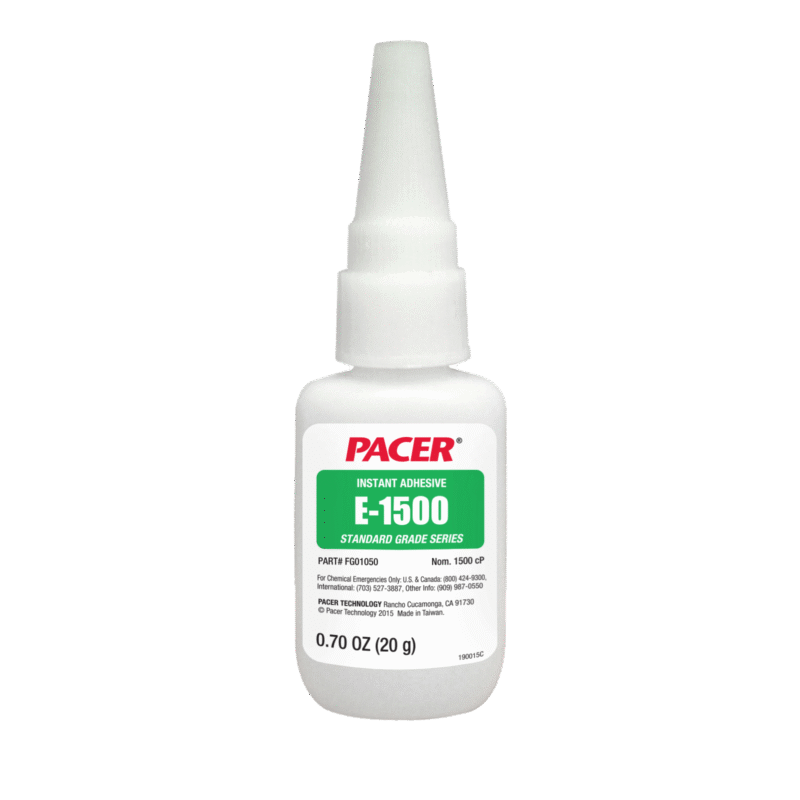
- Pacer E-1500 Instant Adhesive (1300-1700 cP), thickest grade in the E Series, holds position far better on vertical joints, .010 in gap, 20 gram bottle only
- Pacer RX-100 Range Extended (80-120 cP), same viscosity as E-100 but non-surface-sensitive, for porous, acidic, or contaminated substrates
- Pacer RX-50M Gel, a true gel for vertical and overhead joints
- Pacer Premium Acetone Accelerator, speeds full cure through larger gaps
- All cyanoacrylate instant adhesives
Frequently Asked Questions
What is Pacer E-100 used for?
Pacer E-100 is used for general purpose instant bonding of plastics, rubber, metal, and ceramic parts in production assembly, rework, and repair. At 80 to 120 cP it sits in the middle of Pacer’s E Series, which makes it the default pick when you don’t need water-thin penetration or a thicker gap-filling grade, and the one grade to stock if you only want one. It’s sold in 20 gram (0.70 oz) and 1 lb (453 g) bottles.
What materials does Pacer E-100 bond?
Pacer E-100 bonds plastics, rubber, metal, and ceramic. In ASTM D1002 testing it gives 2400 psi tensile shear on steel and 1600 psi on aluminum, and on ABS, nylon, rigid PVC, and SBR the substrate fails before the bond does. EPDM comes in at 100 psi, so plan EPDM joints around that number. For porous, acidic, or contaminated surfaces where a standard cyanoacrylate struggles, Pacer’s RX Series is the non-surface-sensitive option.
Is Pacer E-100 the same thing as super glue?
Yes. Cyanoacrylate, CA glue, instant adhesive, and super glue all describe the same chemistry, and E-100 is an ethyl cyanoacrylate. Pacer Technology is the former Super Glue Corporation. What separates an industrial grade like E-100 from a hardware store tube is a published viscosity band, a stated gap capability, spec compliance data, full physical property testing, and bottle sizes built for repeat production use.
Which Pacer E Series grade should I choose?
Start with your fit-up, not the strength numbers. If the parts already fit tightly and are assembled, use E-5 and wick it in. If the fit is ordinary and the joint is loaded, E-40 is the strongest grade at 4700 psi tensile. If you want one grade that handles a mix of parts, E-100 and its .005 in gap is the default. If the gap is visible or the joint is vertical, go to E-1500 at .010 in. A properly filled joint in the right grade always beats a starved joint in a stronger one.
How much gap will Pacer E-100 fill, and will it run on a vertical joint?
Typical gap capability is .005 in, and yes, at 80 to 120 cP it will run on a vertical or overhead surface before it cures. Medium viscosity in a cyanoacrylate means medium relative to water-thin, not non-sag. If gravity is a factor you have three moves: fixture the part flat, mist with a Pacer accelerator to set the surface before it moves, or change grades. E-1500 at 1300 to 1700 cP is rated to .010 in and holds position much better, and RX-50M Gel is a true gel that stays exactly where you put it.
Does Pacer E-100 meet MIL-A-46050C?
Yes. Pacer lists E-100 as meeting MIL-A-46050C Type II, Class 2 and A-A-3097 (Commercial Spec) Type II, Class 2. The class tracks viscosity, which is why E-5 and E-40 fall under Class 1 and E-1500 falls under Class 3. If your job needs a certificate of conformance, ask for it when you order.
Can I use an accelerator with Pacer E-100?
Yes, Pacer accelerators for instant adhesives are compatible and are used to speed full cure through larger gaps. Two things to plan around. Accelerator applied over exposed adhesive can leave a white frost on the part, called chlorosis, which usually comes off with Pacer X-9 Debonder on a cotton swab. And overall cure strength can drop when accelerators are used. Test on actual parts before you commit a production process to it.
How should Pacer E-100 be stored, and what is the shelf life?
Refrigerate unopened bottles at 40F (4C) for best results, then let the adhesive come up to room temperature before opening. Opening a cold bottle pulls condensation into the material. Once opened, store in a cool, dry location. Stored that way, expect a one year shelf life.
Questions on Fit
Questions on fit for your bonding process? Call (800) 220-1966 or email [email protected].


Reviews
There are no reviews yet.